Inflatable Seal Ball Segment Valve Factory for Precision Flow Control Solutions
2026-10-17
Valves rarely get attention until they leak, jam, or wear out prematurely. At AVM, we build inflatable seal ball segment valves differently—starting with the factory floor where precision flow control is engineered rather than assumed. You'll see how material choices, seal inflation dynamics, and segment geometry come together to handle tough fluids without constant maintenance. If you've ever wondered why two valves with similar specs perform worlds apart, the answer often lies in the details we're about to break down.
How Inflatable Seals Deliver a Bubble-Tight Shutoff Without High Torque
Unlike conventional compression seals that rely on mechanical force to crush a gasket or O-ring, inflatable seals work by pressurizing a hollow profile. When air or fluid enters the seal cavity, the profile expands outward and conforms to the mating surface, filling minute irregularities and creating a uniform contact band. This expansion happens at relatively low operating pressures—often just a few psi—so the sealing force comes from internal pressure, not from tightening bolts or applying high torque. The result is a reliable bubble-tight shutoff even on large or irregularly shaped openings where traditional clamping would be impractical.
The absence of high torque requirements also means less strain on surrounding components. Doors, lids, and access panels can be closed with simple latches or even pneumatic cylinders that hold position, rather than heavy hand wheels or multiple bolt patterns. For equipment that cycles frequently—such as glove boxes, isolation valves, and processing chambers—this reduces operator fatigue and speeds up the cycle time. Because the seal retracts when pressure is released, parts can be moved apart easily, and there is no risk of the seal being torn or abraded by sliding contact during opening and closing.
In practice, inflatable seals find use in applications where contamination control and gentle handling are critical, such as pharmaceutical isolators, food processing equipment, and semiconductor wafer handling. The low mechanical force means that fragile glass, thin metal flanges, or plastic components won't distort. Maintenance is simplified as well: replacing an inflatable seal typically involves loosening a few simple fasteners, without the need to re-torque a complex pattern to achieve the original seal. This combination of bubble-tight performance and low operating effort sets inflatable seals apart from traditional compression methods.
The Impact of Segment Contour Design on Flow Characteristic Curves
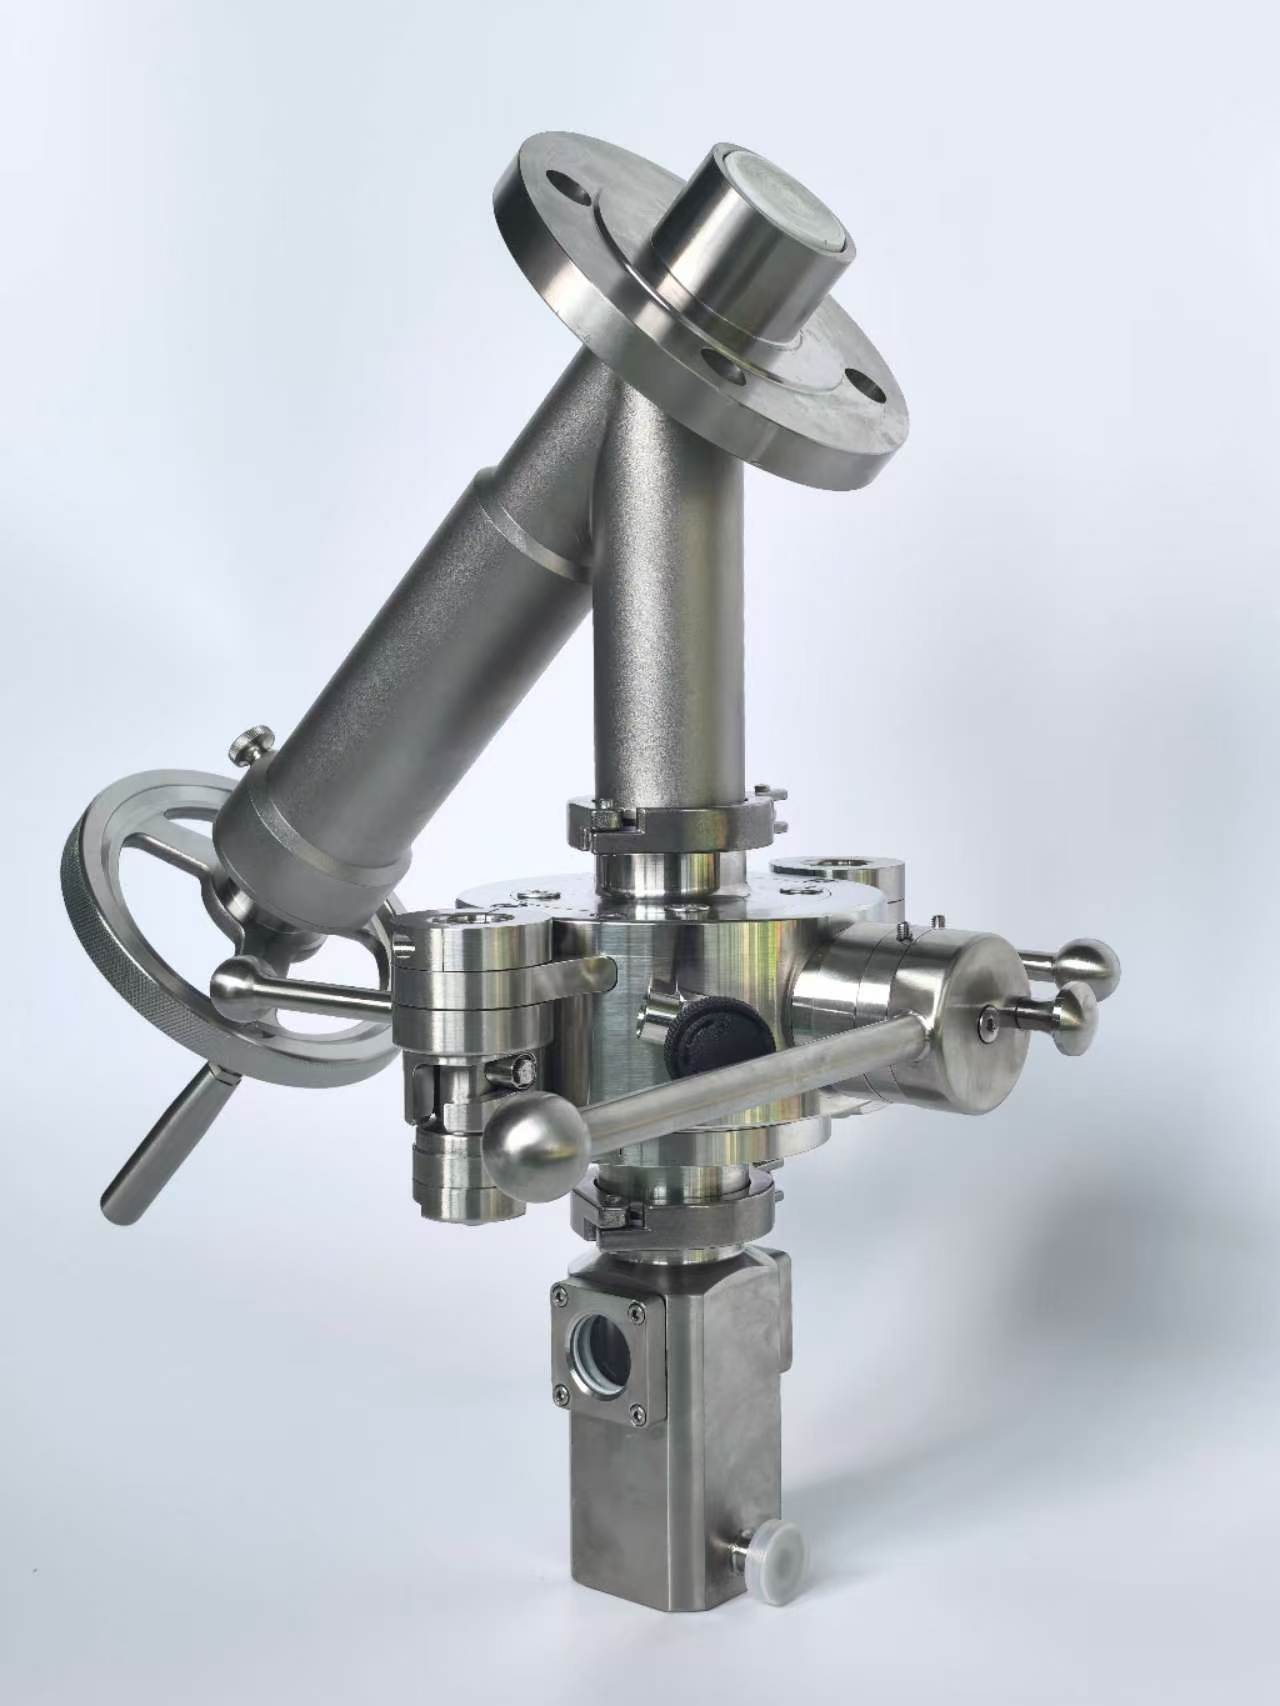
The geometry of a valve segment's leading edge and surface profile directly reshapes the relationship between stem rotation and effective flow area. A flat or gently tapered contour tends to produce a more gradual opening, yielding a modified linear or equal-percentage curve, whereas a pronounced V-shaped or contoured cutout can compress the usable control range into a narrower band. This shift becomes visible in the slope of the installed flow characteristic, particularly at low openings where small angular changes produce disproportionately large flow gains.
Beyond the basic opening curve, segment contour also influences local velocity distribution and pressure recovery. Sharp edges or abrupt contour transitions encourage flow separation and can steepen the curve while introducing instability at mid-stroke positions. By contrast, a smoothly blended profile reduces vena contracta effects and flattens the high-flow end, making the valve easier to tune in closed-loop service. The exact contour chosen thus dictates not only the rated capacity but also how predictably the flow responds across the full travel.
Matching Seal Materials to Process Media for Long-Term Reliability
A seal that survives a short chemical immersion test can still fail after months in service because the process stream rarely behaves like a clean single-component fluid. Trace acids, cleaning agents, or even water absorbed during steam-outs can attack a polymer that looked fine on the datasheet. For example, EPDM handles many dilute acids and ketones reasonably well, but it swells rapidly in mineral oils and hydrocarbon solvents, while FKM resists those hydrocarbons but breaks down in hot water, steam, and some amines. Matching starts with identifying not just the primary chemical but every species that can enter the seal environment, including byproducts and temperature-dependent contaminants.
Temperature shifts the picture more than most compatibility charts admit. A material that is stable at ambient temperature can lose cross-link density or undergo dehydrofluorination at process temperatures. Perfluoroelastomers (FFKM) and PTFE-based seals often solve aggressive chemical and high-temperature combinations, but they carry cost and sometimes lack the resilience of lower-cost elastomers. In cyclic operations, the combined effect of thermal expansion, pressure extrusion, and chemical attack creates failure modes that no single-property test captures. Compression set, explosive decompression resistance, and extrusion gap tolerance all need to be evaluated together rather than in isolation.
Long-term reliability comes from validating the seal in the actual process environment, not from relying on general compatibility tables. Even small differences in filler, cure system, or post-curing can change performance enough to matter. Pilot-scale exposure tests, hardness and volume change measurements over time, and post-test inspection for cracks or surface tack give a better picture than a pass/fail immersion. When a seal shows early signs of softening, shrinking, or leakage at start-up, it is usually a sign that the media mixture differs from the assumed composition. Tracking those field observations back to material selection prevents recurring leakage and unplanned downtime.
What Factory Acceptance Tests Reveal About Valve Performance
Factory acceptance tests cut through the marketing gloss and expose how a valve actually behaves when bolted into a test stand. You learn whether the seat seals at the claimed differential pressure, how much torque the stem needs before the packing starts to weep, and whether the stroke times match what the datasheet promised. These numbers rarely align perfectly with catalog specs, and the gaps tell you more than the pass/fail stamp ever will.
Beyond basic leak rates and shell integrity, a well-run FAT uncovers operational quirks that only show up under load. The valve might chatter during partial stroke testing, or its positioner might overshoot on small signal changes. Watching the actuator cycle a few hundred times reveals whether the gain settings drift, whether limit switches bounce, and whether internal clearances tighten as temperature rises. These are the details that maintenance crews curse later if nobody bothered to look during acceptance.
Ultimately, the FAT is less about proving the valve meets the purchase order and more about establishing a baseline for its entire service life. Vibration signatures, breakaway torque, response curves, and seat tightness readings captured at the factory become the reference points for future diagnostics. A valve that passes with mediocre but stable values will often outperform one that barely squeaks through with ideal static numbers, because the test reveals how the assembly behaves under stress rather than how it looks on paper.
Configuring Valve Ports and Actuation for Non-Standard Applications
When a valve ends up in a skid where standard NPT threads and centered ports simply do not fit, the configuration conversation shifts quickly. Port locations may need to move to the side, angle downward, or accept a flanged adapter that was never in the catalog cut sheet. I have seen more than one installation where the real fix was not a different valve body, but a port block machined to match an existing manifold footprint. That kind of detail rarely shows up in a general arrangement drawing until someone asks why the tubing run looks forced.
Actuation for non-standard applications tends to break into two camps: either the available air supply is too low for a spring return to work reliably, or the process demands a failure mode that a standard actuator cannot deliver without extra hardware. A double-acting cylinder with a pilot-operated check valve can hold position during a pressure drop, but only if the exhaust path is throttled rather than left wide open. For spring-return setups, using a heavier spring means accepting a larger actuator and often a different mounting bracket. Choosing the wrong one leads to sluggish stroking or a valve that never fully seats.
Before the valve is bolted in, walk the port identification against the P&ID, then match the actuator orientation to the available space. Exhaust ports should point away from walkways and any area where moisture could collect inside the silencer. If the valve will spend most of its life throttling rather than just opening and closing, consider a characterized port or a positioner with a custom cam profile. These are not exotic upgrades; they are what make a non-standard valve behave like it was designed for the loop from the start.
Extending Seal Life Through Proper Installation and Routine Checks
Most seal failures can be traced back to the first few minutes of installation. A seal that is forced over sharp threads or pushed into a dirty groove may look fine on the outside but already carries scratches or micro-tears that widen under pressure. Using dedicated installation sleeves, cleaning the housing bore with a lint-free wipe, and checking the shaft for burrs before sliding the seal into place adds only a few minutes to the job but can double or triple the working life of the component. Equally important is verifying that the seal is seated square; a slight tilt forces one side of the lip to bear the full load, leading to uneven wear and early leakage.
Routine checks should go beyond a quick glance for drips. Run a finger along the seal area when the equipment is cool to detect hardening, cracking, or a glassy glaze that signals heat aging. Measure the compression set of removed seals during scheduled downtime—if the lip no longer springs back to its original shape, it has lost the ability to follow shaft movement. For dynamic applications, pay attention to shaft surface finish and lubrication film. A polished, mirror-like shaft can prevent the seal from maintaining a proper lubricant layer, while roughness above the recommended range acts like sandpaper on the lip. Recording these observations over time helps spot gradual changes before a full failure occurs.
Finally, treat installation and inspection as two halves of the same practice. When a seal is removed for any reason, do not automatically reinstall it. Check the wear pattern on the lip: a wide, even contact band usually indicates healthy alignment, while a narrow or off-center band points to misalignment or excessive shaft runout. Replace any seal that shows signs of swelling from incompatible fluids or permanent deformation from overtightening. Pair these visual and tactile checks with simple measurements of radial force or lip tension if the budget allows. The goal is not to inspect more often, but to inspect with a specific purpose, catching the small shifts in material and geometry that signal the end of a seal's useful life before it becomes a costly leak.
FAQ
Our valves use a specialized inflatable seal that conforms to the segment ball, eliminating leakage even under low-pressure differentials. Each unit is machined in-house and tested with air and water before shipping, so you get consistent shutoff without the usual wear points.
These are common in chemical processing, mineral slurries, paper stock, and wastewater treatment. Anywhere sticky or abrasive media would jam a conventional valve, the inflatable seal lets the segment ball rotate freely and then seal tight when needed.
Yes. We build flanged, threaded, or wafer-style connections from 2 inch up to 24 inch, and we can match ANSI, DIN, or JIS patterns. Actuation options include manual gear, pneumatic, electric, or hydraulic.
The seal inflates only when the valve closes, so it avoids constant rubbing against the ball segment during rotation. That greatly reduces seal wear in slurry or powder service, and when replacement is needed, the seal cartridge swaps out without removing the valve body from the line.
Every valve gets a shell pressure test, a seat leak test with the seal inflated at low and high pressure, and a full stroke cycle check. We also provide a test certificate with serial number traceability for each order.
We keep seal kits in stock for all our models and can ship within a few days. Our engineers can walk your maintenance team through a rebuild over a video call or visit if the line is critical.
We hold inventory of common body castings and seal profiles, and our in-house CNC and rubber molding cells let us shift production quickly. Typical lead time is four to six weeks, with rush options for breakdowns.
Conclusion
At the heart of these precision flow control valves is an inflatable seal that expands against the ball segment, creating a bubble-tight shutoff without demanding high torque from the actuator. This design keeps operating forces low while handling everything from clean gases to abrasive slurries. Segment contour geometry plays an equally critical role: subtle changes in the sealing edge or ball curvature reshape the valve's inherent flow characteristic, letting engineers dial in linear, equal-percentage, or custom curves that match loop dynamics. Matching the seal elastomer to the process media—whether it's aggressive chemicals, high-temperature steam, or food-grade fluids—prevents swelling, cracking, and premature leakage, extending service intervals far beyond conventional metal-seated designs.
A rigorous factory acceptance test is more than a formality. It maps actual flow coefficients across the full travel range, verifies seal inflation and deflation cycles under rated pressure, and documents leakage rates using helium or water. For non-standard applications—odd port orientations, dual-seal arrangements, spring-return actuation, or low-flow trims—the factory configures each valve at the component level before assembly, avoiding expensive field modifications. Once installed, proper alignment and periodic checks of the inflation pressure, seal wear indicators, and actuator stroke keep the valve performing like new. Routine seal replacement becomes a planned event rather than an emergency shutdown, which is why these inflatable seal ball segment valves remain the go-to solution for plants that cannot afford unplanned downtime.
Contact Us
Contact Person: Ananda
Email: [email protected]
Tel/WhatsApp: 8619016718200
Website: https://www.wzaomi.com