Professional Die Making Steel Rule Manual Bender: The Complete Guide to Precision Bending
2026-10-24
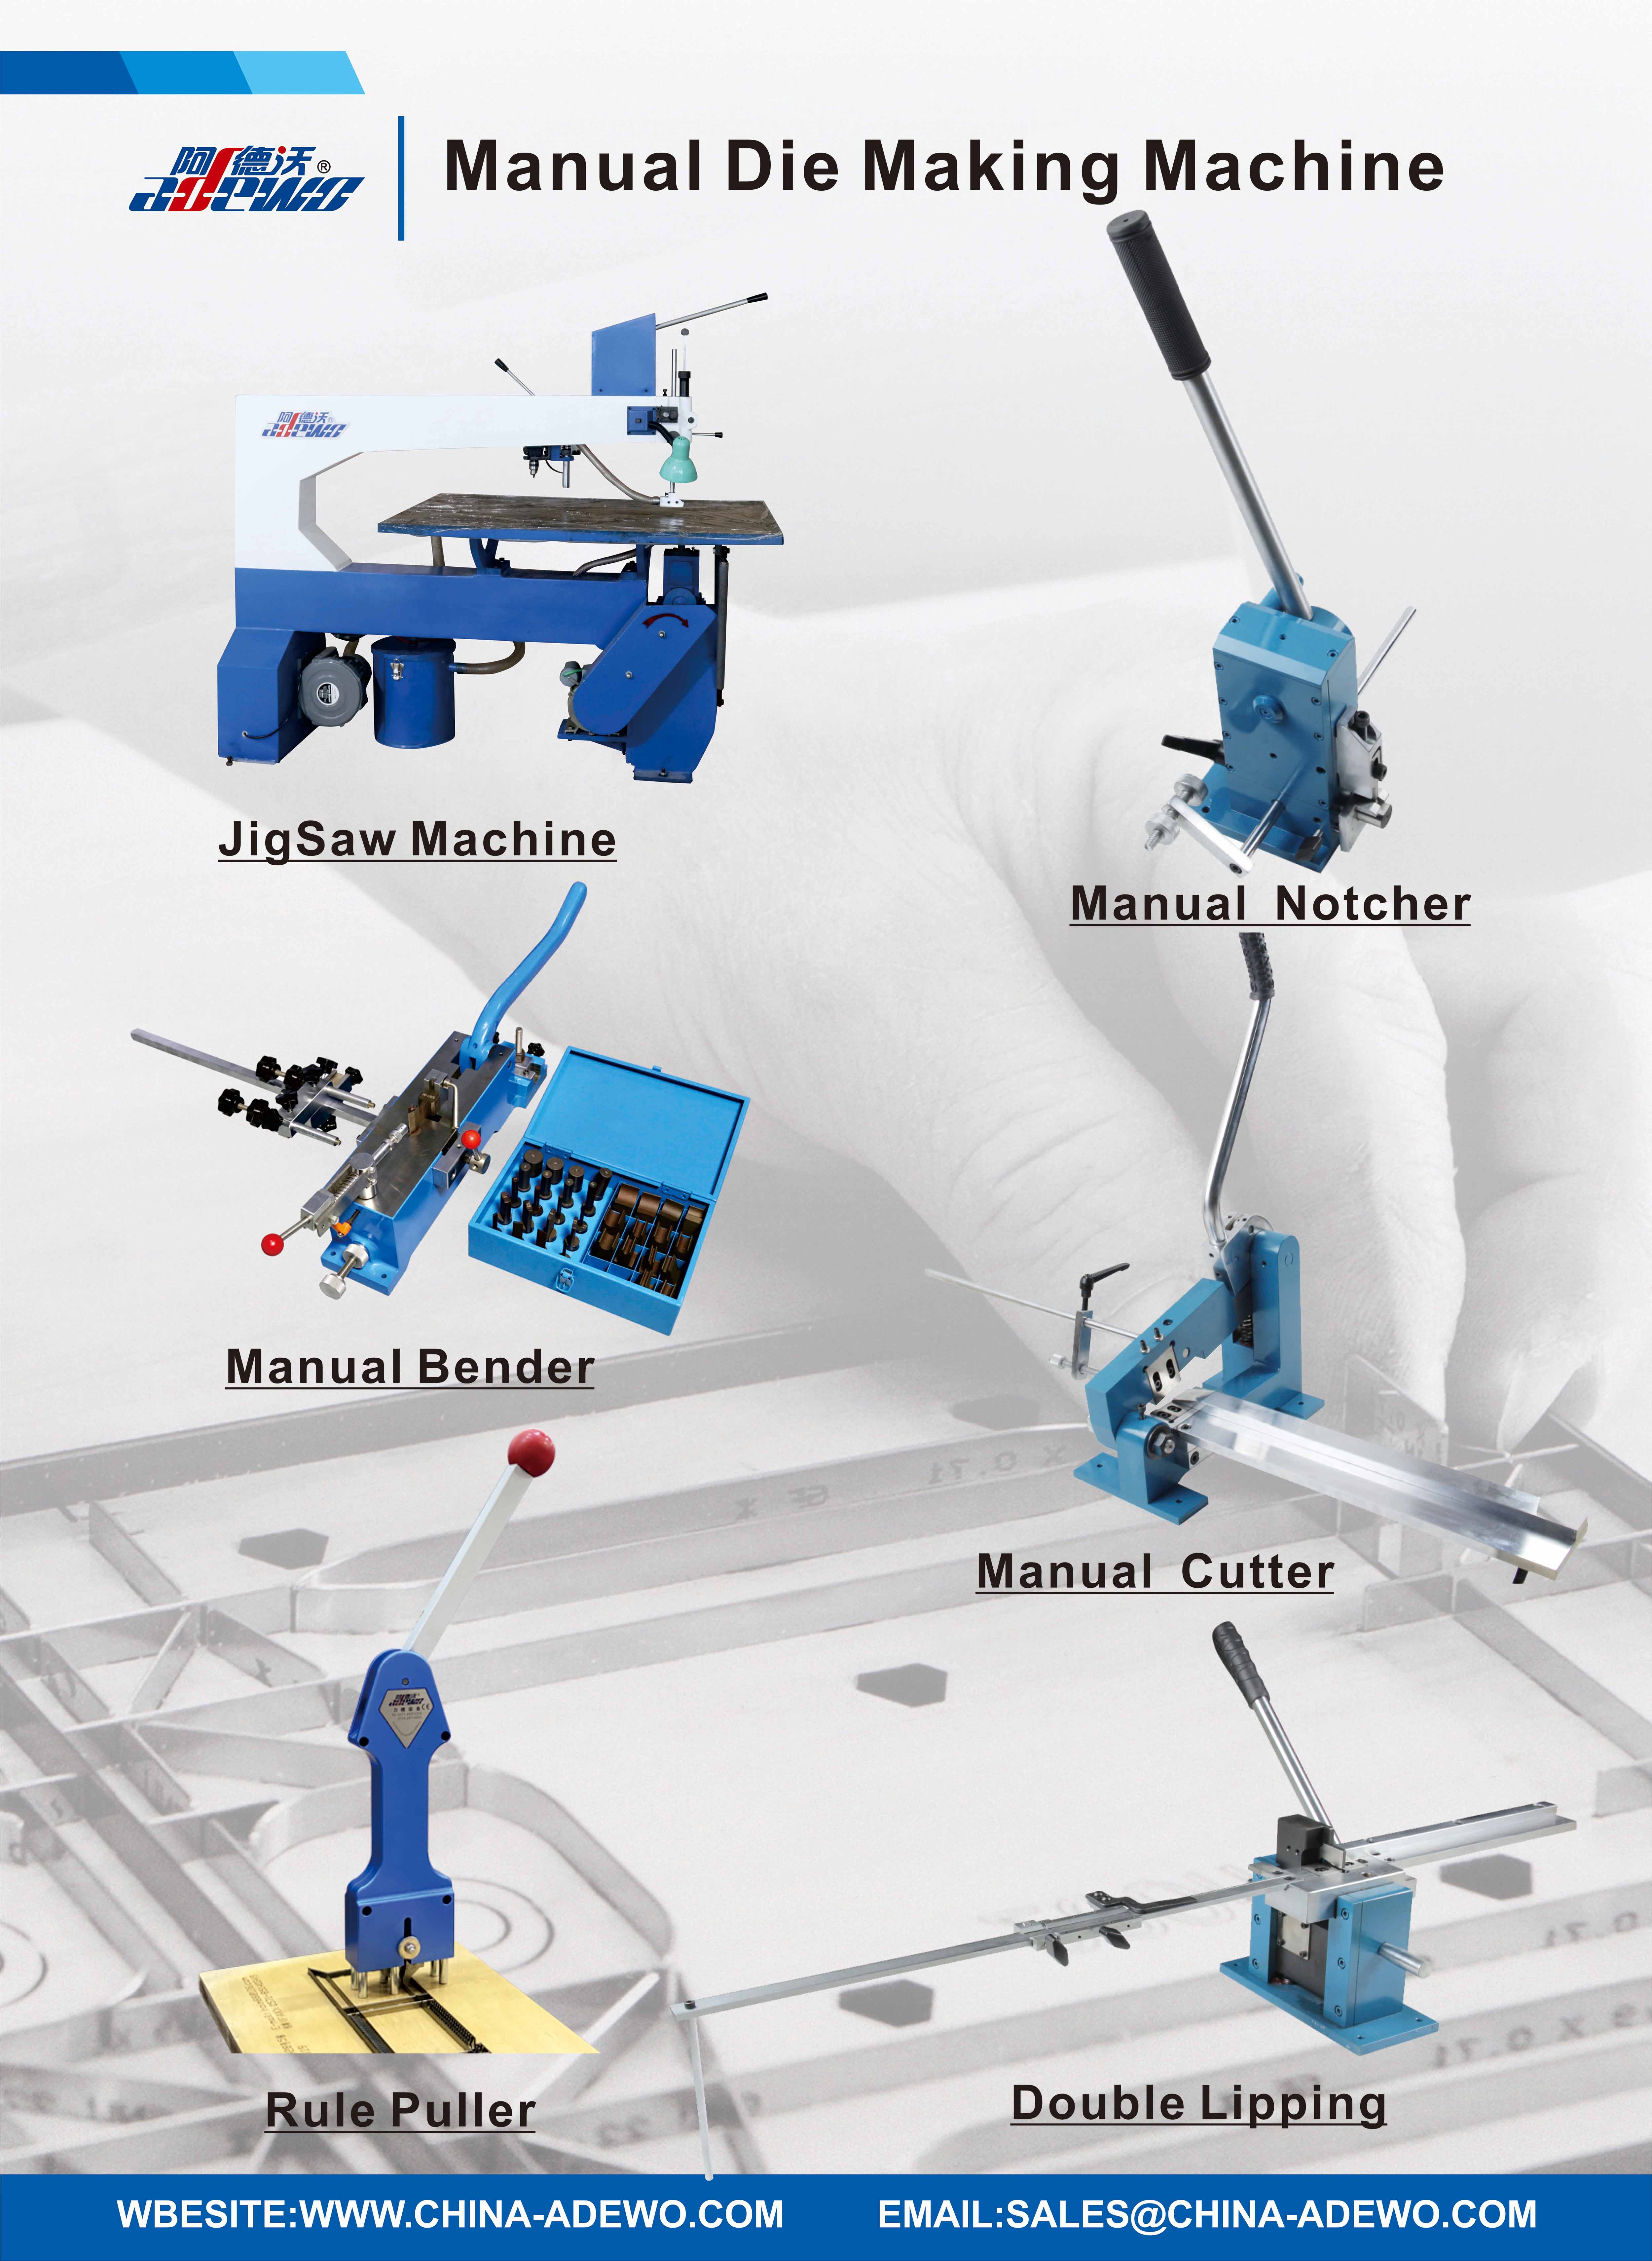
If you’ve ever fought a steel rule that refuses to hold its radius, you know manual bending is anything but simple. Professional die making demands a level of accuracy that most generic advice skips over. In this guide, we get into the details that actually matter: material behavior, bend sequencing, and the subtle technique shifts that separate clean profiles from scrap. Along the way, you’ll see why tools from ADEWO have become a quiet benchmark for shops that take precision seriously—and how the right manual bender changes what’s possible.
Reading Bend Allowance Before You Pull the Handle
Most operators skip the bend allowance table until a part comes out short or over-bent, then they scramble to reverse-engineer the mistake. But if you take thirty seconds to read the allowance stamped on the die or printed on the setup sheet before you start the stroke, you can catch mismatched material thickness, wrong V-opening, or a dull punch that will ruin the flange length. The numbers are not just reference—they are the difference between a clean first hit and a scrap bin full of guesswork.
On a press brake, the bend allowance changes with grain direction, temper, and even the coating on the sheet. A cold-rolled 16-gauge may bend short by 0.008 inch when the grain runs parallel to the brake, while the same part cut across the grain needs an extra 0.015. If you pull the handle without checking the allowance against the actual stock in your hands, you get a surprise at inspection. Keep a small laminated chart near the control panel—not the generic one from the manual, but one marked up with your shop's own corrections from past jobs.
Reading the allowance also means reading the bend line, not just the number. A heavy center punch mark or a laser-etched line can shift the bend start by half a material thickness. Before you cycle the ram, run a fingernail along the line and compare it to the backgauge stop. If the stop is set for a theoretical flat pattern but the line is off by more than 0.010, adjust the gauge or the program. That one glance before the handle comes down saves ten minutes of rework after every batch.
Matching Rule Height and Hardness to Your Die Geometry
Rule height only works when it is read against the real clearance in your die, not the nominal board thickness. The moment ejection rubber, chase plates, or curved contours enter the picture, the effective depth changes. A rule that sits too proud tends to deflect under load and produces uneven penetration, while one that is too shallow leaves tags or requires excessive press force on detailed cuts.
Hardness should follow local geometry rather than a single spec for the whole die. Straight runs can tolerate harder, more wear-resistant rule because stress spreads evenly along the edge. Tight radii, short slots, and perforating areas concentrate bending and impact, so a slightly softer rule often survives longer in those spots. Matching temper to the smallest feature on the board prevents brittle failures that harder rule invites.
A practical way to spec both is to break the die into zones. Use a taller, harder rule only where clearance and feature density allow it, and step down height or temper in clustered or curved sections. Run trials on the actual substrate with the same ejection material in place, since compression recovery and board warp will shift the contact point more than a flat CAD layout suggests.
Hand Pressure Tricks for Clean 90-Degree Corners
When you're cutting in along baseboards or crown molding, the way you grip the brush changes everything. Too much pressure causes the bristles to splay and paint to bleed under the tape, while too little leaves a ragged, uneven line. The trick is to load just the lower third of the brush, then press the ferrule lightly between your thumb and index finger as you pull it along the corner. That slight downward force keeps the bristle tips aligned with the edge, letting the paint release in a controlled bead instead of a messy smear.
For drywall corners or trim work, hand pressure on a sanding block or putty knife matters even more. If you're smoothing joint compound into a 90-degree angle, press the blade flat against one face first, then ease it into the corner with your fingers spread wide across the handle—this distributes force evenly and prevents gouging. On the back side, lighten your grip just enough to let the tool ride the existing angle rather than cutting a new one. With practice, your hands learn to read the corner and adjust pressure automatically, which is what produces that crisp, paint-ready line without extra caulk or touch-up.
A common mistake is squeezing the brush or knife at the very end of the handle, which creates a lever effect and amplifies any wobble. Move your grip closer to the working edge and use the heel of your hand as a pivot. For freehand cutting near ceilings, lock your wrist and shift your whole forearm, keeping the brush at a 45-degree angle to the corner. This lets the pressure stay constant while the motion comes from your shoulder, not your fingers, so the line stays dead straight through the corner.
Preventing Springback in Thicker Steel Rules
When you move into thicker steel rule, the material's resistance to permanent deformation climbs fast. A bend that looks perfect in the die often relaxes by a degree or two once the pressure comes off. That elastic recovery, or springback, has to be countered at the tool rather than hoping the rule will stay put on its own.
The most reliable fix is to overbend deliberately. Set the forming stop so the rule passes the target angle while still under load, letting it settle back to where you actually need it. For heavier sections, this usually means bottoming the bend with enough tonnage to plastically stress the entire thickness, not just the outer fibers. Narrowing the die opening also helps because it forces the bend radius tighter and pushes more of the cross-section past the yield point.
Don't overlook the blank itself. Thicker rule is less forgiving of grain direction, so bending across the grain will produce less springback than bending along it. If you're forming a series of identical pieces, keep the setup notes consistent: same die, same penetration, same pause at the bottom of the stroke. A brief dwell under full pressure can make a surprising difference in locking the angle in place.
Jigs and Stops That Turn a Manual Bender into a Repeatable Tool
A bare manual bender relies on the operator's eye and feel, which means two pieces can come out slightly different even when you're trying hard to match them. The simplest upgrade is a stop block that catches the end of the tube at the same point every time. Bolt a small piece of angle iron or a machined stop to the bender's base or the bench next to it, and you'll eliminate most of the guesswork in tube placement before a bend.
For consistent angles, you don't need a digital readout. Attach a pointer to the bending die and place a degree wheel or a printed protractor on the fixed frame. Mark your target angle, then bend until the pointer lines up. If your bender has spring-back, do a test bend first and note the offset between the dial reading and the actual angle you get. A piece of hardwood with a V-groove cut at the desired angle also works as a visual template, letting you bend until the tube sits flush in the groove.
Once you've produced one good part with multiple bends, turn that part into a master. Clamp it to a flat board and screw down small blocks or dowels at a few key locations, like the start of the first bend and the tangent point of the second. For the next tube, slip it against those same stops before each bend. It feels a bit like setting up a production fixture, but the payoff is real: less scrap, faster setup, and the confidence that every part will fit the same way as the first one.
Maintenance Habits That Keep the Pivot Tight and Accurate
Most pivot wear starts quietly. A few thou of play today becomes a visible wobble after a couple hundred cycles, and by then the mating surfaces have usually started to gall. Checking axial and radial movement with a dial indicator every few weeks takes less than ten minutes and gives you a baseline before problems show up in the cut or the reading.
Lubrication is where habits either save the pivot or slowly kill it. Too much grease attracts fines that lap the bearing surfaces; too little lets the contact patch run dry under load. A light, consistent film applied after cleaning is usually enough. Wipe the old lubricant off completely before adding fresh, otherwise you're just mixing abrasive paste in place.
Fastener tension matters more than most people admit. Overtightening the clamping bolts distorts the bore and pinches the pivot, while undertightening lets the assembly shift under vibration. Use a torque wrench and stick to the manufacturer's range, then recheck after the first few hours of work. A simple paint mark across the bolt head and housing makes any movement obvious at a glance.
FAQ
It gives you the leverage and control to form hardened steel rule by hand, letting you hit tight radii without cracking the strip, which is essential for cutting dies.
A well-built manual bender can hold tolerances within a few thousandths when you use the stops and gauges consistently, but the real limit usually comes down to how carefully you set up each bend.
Look at the maximum rule height and thickness it can handle, whether the bending head adjusts to different angles, the quality of the clamping jaws, and how easy it is to replace wear parts.
Many can, but you may need to swap or adjust the forming rollers and guides for different heights, thicknesses, or hardness levels to avoid slipping or scoring the rule.
Forcing a bend too quickly, using worn rollers, ignoring changes in rule hardness, and not locking the workpiece firmly can all introduce springback variation and position drift.
For daily production use, clean and lightly lubricate the moving parts every shift and inspect the rollers and clamping surfaces weekly for grooves, chips, or play that affect alignment.
It often is for short runs and custom die work because it gives immediate feel and control, costs less, and takes up little space, though powered machines win on high-volume repeatability.
Keep your fingers clear of the pinch points, clamp the machine to a stable bench, and make sure the rule is supported so it cannot whip around when you apply force.
Conclusion
Precision bending on a manual bender starts well before you pull the handle. You need to know exactly how much material will stretch and compress along the bend line, so you can position the rule correctly and avoid ending up with a dimension that's off by half a millimeter. That allowance changes with rule height and hardness, and matching those two factors to your die geometry keeps the steel from cracking or buckling under pressure. When you're forming a 90-degree corner, the way you apply hand pressure matters just as much as the setup. A quick, jerky pull tends to leave a rounded edge or a slight twist, while steady, even force through the full stroke gives you a crisp corner. For thicker rules, springback becomes a real headache; you can compensate by overbending a few degrees and then easing back, or by using a secondary tap with a soft mallet right at the bend line.
If you're going to bend more than a handful of rules, jigs and stops are what turn a manual bender from a one-off tool into something repeatable. Set a stop for the blank length, clamp a small guide for the bend location, and every piece comes out the same without you having to eyeball each one. This is especially useful when you're making identical cutting dies for packaging or gaskets. Over time, the pivot point on any manual bender will wear if you ignore it. A loose pivot lets the bending arm shift sideways, and suddenly your supposedly accurate 90-degree bends are drifting to 88 or 92 degrees. Keep the pivot tightened to the manufacturer's spec, clean out any metal dust after each session, and add a drop of light oil to the moving parts. If you feel any play or roughness in the stroke, address it before it affects your work.
Contact Us
Contact Person: KAELYN LEE
Email: [email protected]
Tel/WhatsApp: +86 15012673758
Website: https://www.china-adewo.com