Top 3D TPU Heat Transfer Label Supplier for Durable Custom Apparel Branding
2026-10-09
When it comes to custom apparel, the label is often the last detail brands consider, yet it can make or break a garment’s perceived quality. Peeling, fading, or uncomfortable tags quickly undermine customer trust. That’s where a reliable 3D TPU heat transfer label makes all the difference. As a top supplier in this niche, Victorygen heat transfer label delivers durable, high-definition branding that survives countless washes and wears. If you’re ready to elevate your apparel line with labels that actually last, keep reading.
Why Raised TPU Logos Feel More Premium on Cotton and Poly Blends
There’s a subtle shift in how a garment reads when the logo sits above the fabric instead of sinking into it. Raised TPU gives that slight dimensional lift, and on cotton-poly blends it creates a clean break between the soft, matte surface of the shirt and the smooth, almost rubberized lettering. The touch becomes part of the experience—fingers catch the edge of the mark just enough to register it as intentional, not printed as an afterthought.
Cotton and poly blends tend to have a slight heathering or uneven texture up close, which can swallow flat prints. A raised TPU logo holds its own against that variation. It reads as a separate layer, with a subtle gloss that contrasts the fabric’s low luster. That contrast makes the logo feel considered, like hardware on a well-built bag rather than decoration added later.
There’s also a durability signal at play. TPU won’t crack or fade the way some thin screen prints do after repeated washing, and the raised surface keeps its shape even as the fabric softens over time. That resilience quietly reinforces the idea of quality—not because it shouts, but because it stays crisp long after flat prints have started to break down.
What Separates a True 3D Heat Transfer from Flat Screen Print
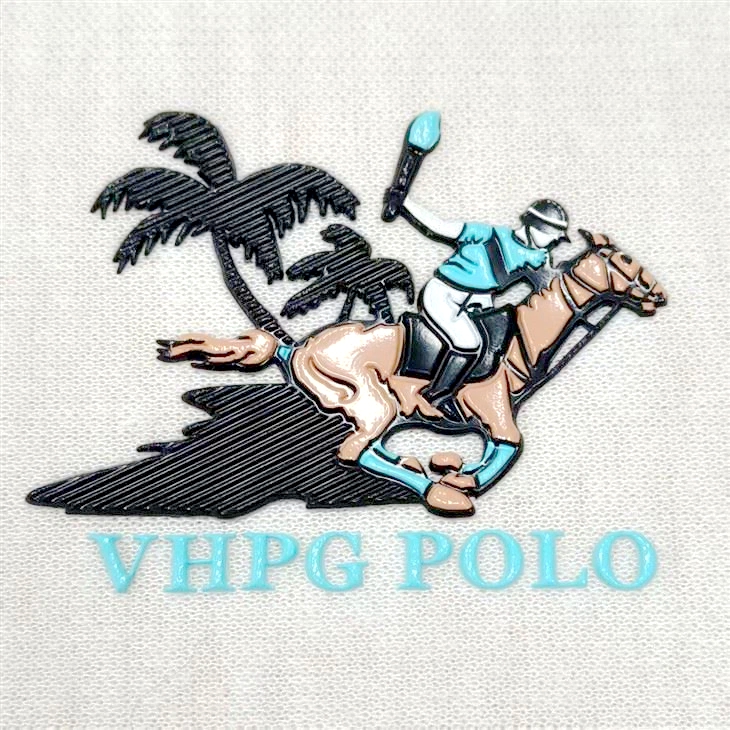
Flat screen prints sit on the surface. You can feel the ink layer, but it’s uniform—same thickness across the design, no real dimension. A true 3D heat transfer changes that entirely. The raised areas aren’t just a thicker ink deposit; they’re built through a specialized gel or puff additive that expands under heat, creating a tactile, embossed profile you can run your finger over. That physical depth is the first clue you’re dealing with something more than a standard print.
The difference also shows up in durability and flexibility. Flat prints can crack or fade after repeated stretching and washing, especially on performance fabrics. A proper 3D transfer needs to bond into the fabric while holding its raised shape, which demands a different resin system and curing window. It’s not merely about looking raised—it has to survive real wear without peeling or flattening. If the texture disappears after a few washes, it was never a true 3D transfer to begin with.
There’s also a matter of edge quality. Flat screen prints often have a slight halo or uneven edge where the squeegee dragged ink. A genuine 3D heat transfer should have crisp, clean borders that rise sharply from the garment, almost like a molded badge. That precision comes from the transfer process, not from layering more ink on a screen. So when you compare them side by side, the real 3D option feels less like a print and more like a component attached to the fabric.
How the Right Supplier Shortens Sampling Without Extra Fees
A dependable supplier doesn't ask you to wait weeks just to see a first sample. They already have the fabrics, trims, and machinery lined up from past production runs, so the sampling phase becomes a fast, focused exercise instead of a long back-and-forth. You send one clear spec sheet, and they pull from existing stock, cut the pattern the same day, and stitch a sample within 48 to 72 hours. No extra charge for rushing, because they aren't starting from zero — they're reusing what they've already mastered.
Short sampling without extra fees comes down to how well the supplier manages its internal workflow. A good partner keeps a small in-house team dedicated only to samples, so your project doesn't get queued behind bulk orders. They also maintain a library of standard components — zippers, buttons, linings, elastics — that can be swapped in instantly. When you request a change, they don't re-quote or start over; they simply make the revision on the existing sample and send a photo or video for approval within a day. That's the difference between a supplier who understands product development and one who treats sampling as a separate profit center.
The real trick is communication. Instead of formal emails and multi-day waits, the right supplier uses quick chat tools, annotated photos, and short video clips to confirm details before cutting. They ask the right questions up front — seam allowance, stitch density, label placement — so you don't pay for avoidable remakes. And because they value the long-term manufacturing contract, they absorb the small cost of a fast sample as part of building trust. You get a sample in your hand while your competitors are still waiting for a quote.
Heat Press Profiles That Prevent Edge Lift After Repeated Washes
Edge lift rarely starts at the press—it starts with how the adhesive film is cut and how the fabric is prepped. If the transfer extends all the way to the hem or seam, even a perfect cure will curl once the garment shrinks in the dryer. I keep the design at least a quarter inch away from any seam and pre-press the shirt for five seconds to pull moisture out of the fibers before laying the transfer down.
For most poly-blend shirts, I run 320°F for 12 to 15 seconds with firm, even pressure, then let the carrier sheet cool to warm before peeling. A hot peel can stretch the edges just enough to lose the bond. On cotton or thicker fabrics, I raise the dwell to 15 to 18 seconds and add a second press from the back side for 8 seconds after removing the carrier.
The step most people skip is the post-press cure. After the transfer is applied, I cover it with a silicone sheet and press again for 5 seconds. This re-flows the adhesive into the weave and seals the outer edge. Then the shirt hangs for a full 24 hours before the first wash, and I always tell people to wash inside out on cold and skip the dryer for the first cycle. That extra day makes the difference between edges that stay flat and corners that peel by the third wash.
Designing Artwork for Sharp Raised Details on Small Labels
Getting crisp raised detail on a label that barely fits on your fingertip forces you to rethink every stroke. Thin hairlines that look elegant on a proof will often vanish or break once the paper is actually embossed or hit with a hot foil stamp. Keep the smallest line weight above 0.5 point and open up counters in any lettering under 8 point, because the physical stretch of paper or film tends to close gaps that look fine on screen.
Small labels reward restraint. Pick one or two elements to carry the raised effect, and let everything else recede. A sharp edge reads best when it's surrounded by quiet space, not by competing textures. If you're combining raised areas with ink or foil, test how the coating behaves on the tallest points — some materials will crack or pull away if the angle of the bevel is too steep, so a slightly rounded shoulder often holds detail better than a knife-edge.
For production files, keep every raised element on its own labeled layer and build those shapes as solid vectors. Avoid gradients, drop shadows, or opacity tricks in the artwork that defines the raise, because plate makers need clean closed paths to etch or engrave accurately. Before you send anything out, print the label at true size and feel the edges with your fingertip or a loupe; if a detail disappears at that scale, it will not come back once metal meets paper.
Managing Color Consistency Across Dark and Light Fabric Runs
When the same dye lot lands on both deep navy and pale ecru, the usual lab-dip approvals start to feel almost useless. Dark shades hide uneven uptake until they are side by side under retail lighting, while light fabrics expose the faintest shift in temperature or depth. Keeping them aligned means rethinking the order of operations instead of trusting a single final inspection.
We have learned to separate the base calibration for each extreme before mixing anything at scale. For dark runs, the focus goes to saturation limits and how the fiber accepts multiple passes without turning muddy. For light runs, the priority is keeping the undertone clean, since even a trace of residual dye in the machine will nudge ivory toward beige. Small reference strips from each batch stay pinned to the cutting table, so the production team can compare under both cool and warm bulbs without waiting for a lab report.
The practical fix is not chasing absolute matches across the whole range but building a controlled bridge. We pair every dark lot with a lightweight sample from the same base recipe, then adjust the light lot only after checking how the bridge piece reads at the seam. This way the contrast between a black jacket and its cream lining stays deliberate rather than accidental.
FAQ
The raised polyurethane layer resists abrasion, washing, and stretching far better than flat ink prints. Because the design is molded rather than simply printed, it won't crack or peel away from the garment even after dozens of industrial laundry cycles.
Yes. A reliable supplier will work from your vector artwork to cut any outline you need and mix Pantone-matched colors into the TPU material. That means you can replicate a complex logo or a simple wordmark without being limited to stock templates.
The label has a heat-activated adhesive backing. You place it on the fabric and apply pressure with a heat press at a specific temperature for a few seconds. Once cooled, it bonds directly to the fibers and stays put without any stitching.
They work well on cotton, polyester, nylon, and blends. The key is choosing the right adhesive formula and pressure settings for the fabric's surface. Many brands use them on activewear, outerwear, and even accessories like bags and caps because the label flexes with the material.
It varies by manufacturer, but many offer small runs starting around 500 to 1,000 pieces. Some suppliers are willing to accommodate prototypes or sample orders before you commit to a full production batch, which helps when you're testing a new design.
TPU gives a smooth, rubbery, slightly raised texture that feels modern and technical. Embroidery has a stitched, traditional appearance, while woven labels are flat and soft. TPU is often chosen when you want crisp edges, a glossy finish, and a no-thread look that stands up to heavy wear.
Once fully bonded, removal is difficult and may leave adhesive residue or damage the fabric. However, during the first few seconds after pressing while the adhesive is still warm, you can sometimes reposition the label carefully. It's best to test on scrap fabric first to nail the exact time and temperature.
Ask about their material sourcing, whether they use high-grade polyurethane, and how they handle color matching across batches. A good partner will provide physical samples, share detailed application instructions, and offer quality checks at multiple production stages. Communication and willingness to troubleshoot issues matter as much as the base price.
Conclusion
The difference between a flat screen print and a true 3D TPU heat transfer label becomes obvious the first time you run a finger across it. Raised TPU logos add a slight shadow and soft-touch dimension on cotton and poly blends that flat ink simply cannot mimic, especially on small labels where every edge matters. Getting that sharpness from artwork requires more than uploading a vector file; fine details need adjusted stroke weights and open counters so the molded surface doesn't blur during pressing. Color adds another layer of complexity because the same white TPU will look noticeably different on black cotton than on heather grey. A capable supplier compensates with tuned base layers and density changes instead of just resending the same file.
That practical knowledge carries into sampling and production. Some suppliers charge extra for every revision or take weeks to send physical swatches, which stalls a branding project before it starts. The better ones run three or four sampling rounds at no added cost and still deliver within days because their prepress team catches issues in the artwork stage. Heat press settings matter equally: a profile built for a thick poly blend will often leave edge lift on lightweight cotton after a dozen washes. The right supplier adjusts dwell time, pressure, and peel temperature for the specific fabric and label size, then tests washed samples before approving bulk. That is what turns a raised logo from a nice sample into a durable part of the garment.
Contact Us
Contact Person: Wang Song Lin
Email: [email protected]
Tel/WhatsApp: +8613751282193
Website: https://www.heat-transferprinting.com/